 Tech


 IMAGES BY THE AUTHOR
uying an old project is exciting; a new project gets your creative juices flowing, especially if it is something you have wanted for a long time. However, that doesn’t mean that you won’t be scratching your head wondering why someone would do something so dumb. Enter our “Kustom” 1957 3200. This truck was built as a Kustom in the late 1970s/’80s, as evidenced by the lack of wire-feed welds on the big mods, such as the 4-inch top chop (looks great but was executed poorly) and suicide doors, which were brazed with brass rod. At one point it had a flip-forward front clip, but that has been welded shut (with the hardware intact), and the fenders welded to the cab. It is a bit of a mess, but we are up for the challenge.
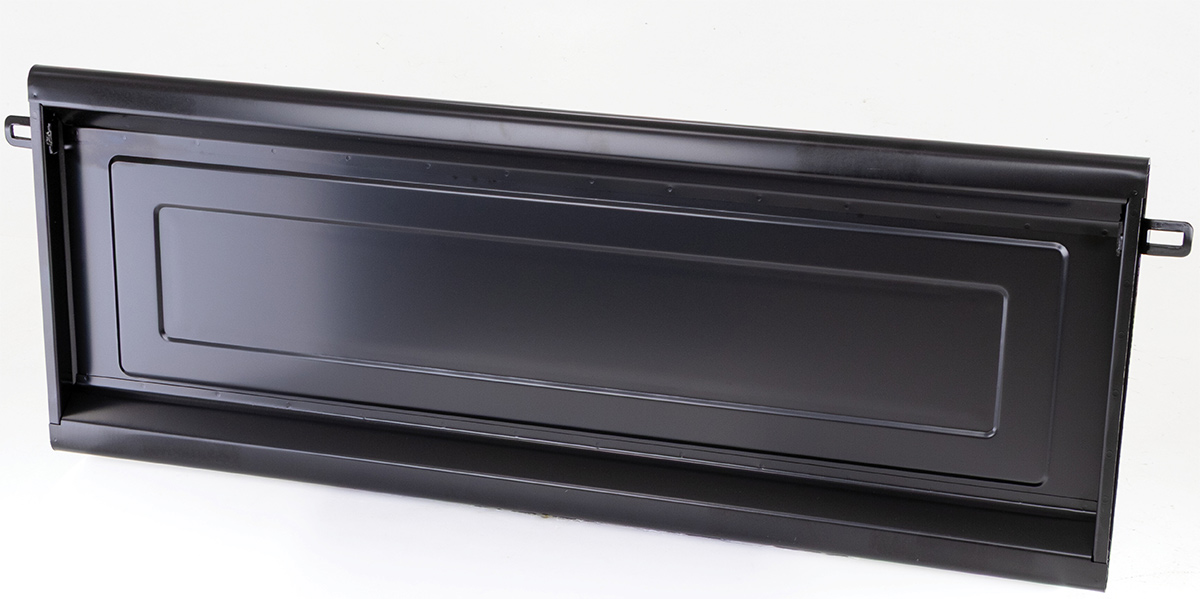
This truck needs a lot of attention. The top chop looks good, but the welds are terrible and they just paved over it with body filler. It doesn’t look as if this truck was ever operational; it has sat in a garage (and eventually a field) for decades, where moisture has crept beneath the filler and caused more issues. That is the first thing we need to tackle: fixing the rust. There are two main areas we are focusing on first: the tailgate and the cab floor.
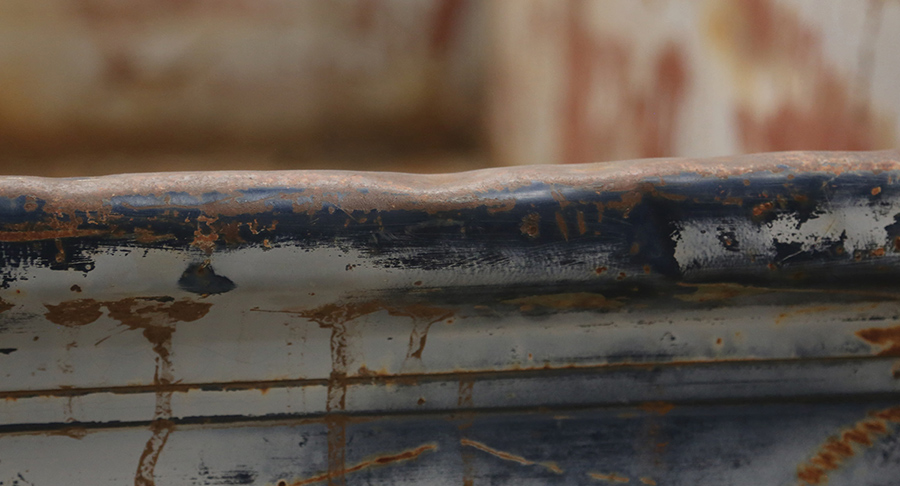
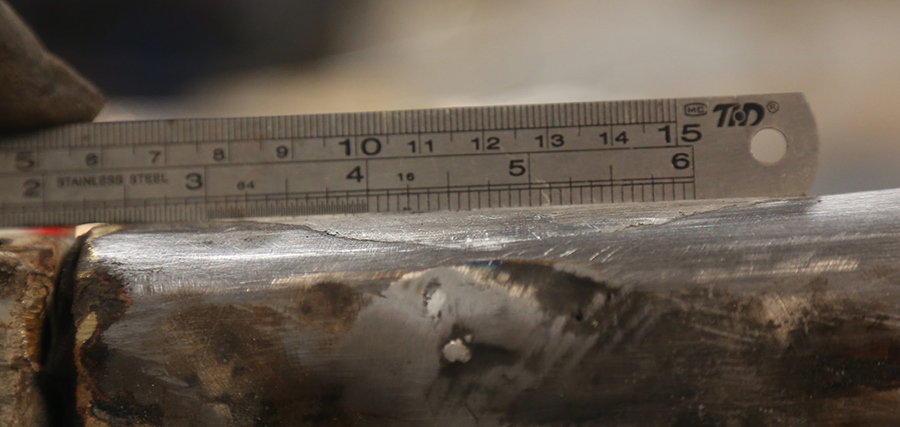
This is the single-most difficult area to repair on a tailgate. Because it is fully rounded over, there is an inherent strength to it, making it harder to get dented and even more difficult to fix said dent. The steel is very thick, about 14-gauge for most models, which is quite tricky to move across a small 1.5-inch radius. Additionally, the radius is not quite fully round; it is more of an offset teardrop. This shape tends to push the flat sides out as the rounded top moves in, making reshaping the rail tough to work.
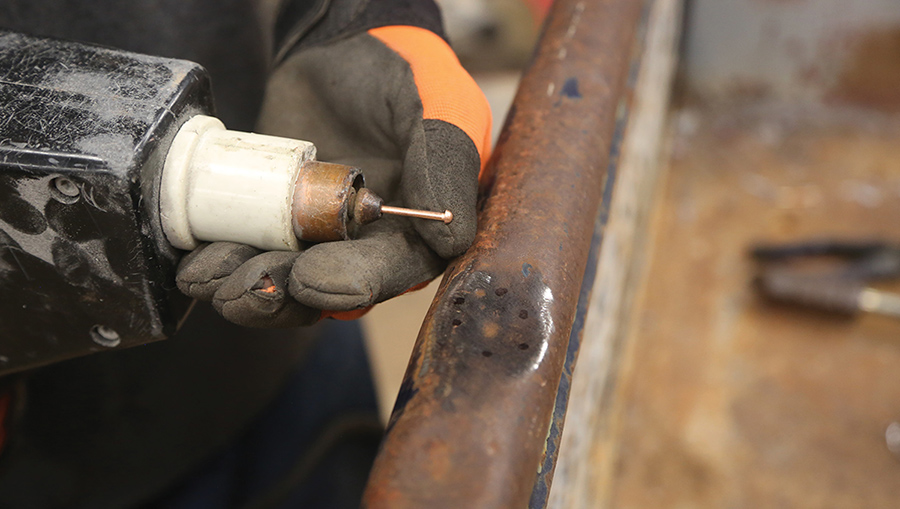
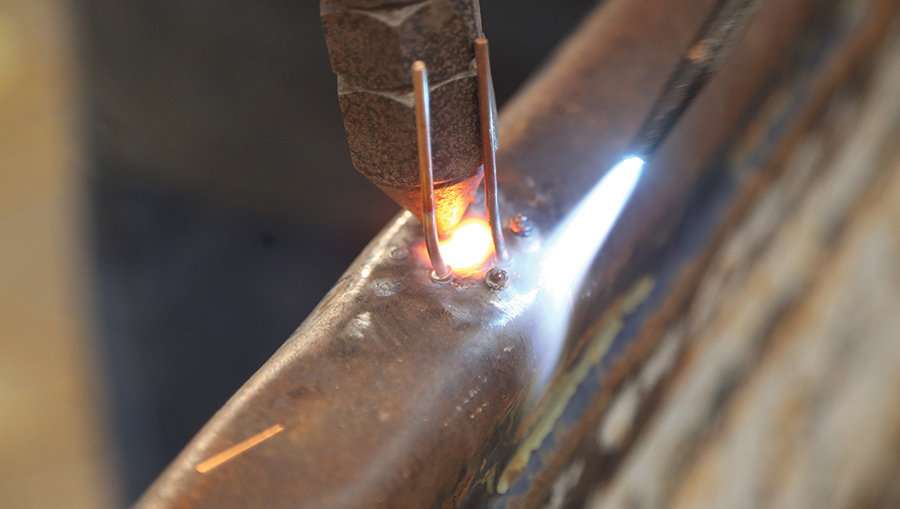
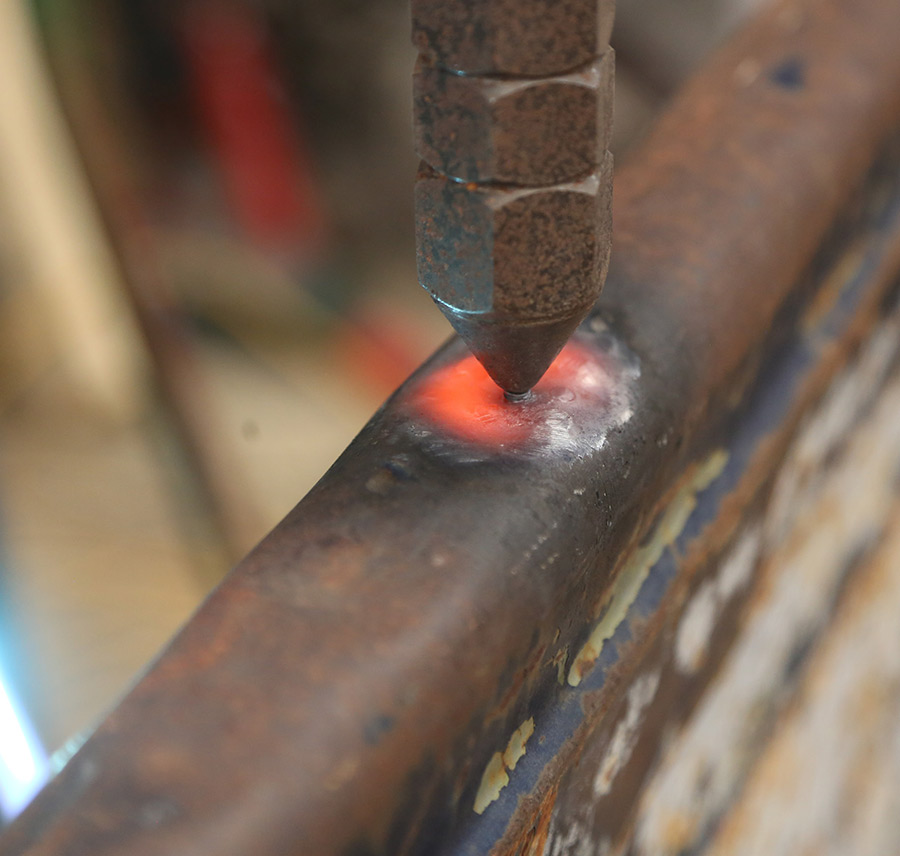
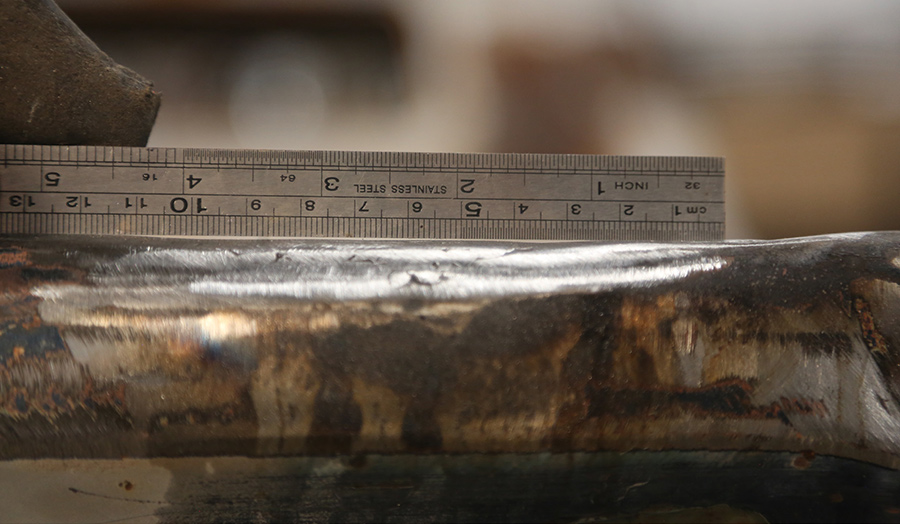
You can’t push the dent from the inside so you got out the stud gun and slide hammer. This is pretty basic stuff, but because the top of the tailgate is rounded, you can’t just slam the slide on the hammer and expect a 1-inch dent in 14-gauge steel to just acquiesce and come back into shape. A little heat from a torch helps convince the thick steel to yield to your demands and move where you want it. We used an oxyacetylene torch set with a rosebud tip to heat only the area we wanted to move, which works quite well. You won’t get it absolutely perfect, but it should be close.
You may be tempted to weld a stud in the center of the dent and pull. For small dents, that can work, but for dents in radiused metal we find it best to work from the outside in. This is because the slide hammer has a tendency to pull a little nipple in the center, which can create other issues. Pulling from the outside of the dent toward the center, the center will naturally come up as you go, reducing how much the metal stretches. As you experiment with your repairs, you will develop your own process.
Adding heat loosens the steel so it will move. The best part is that you control where the heat goes, so you can leave the shallow edges cold and only heat up the deeper areas to get more lift where you want and minimal lift in the cool areas. This is very much an art, but you don’t have to be the Michaelangelo of metal; just remember less is more and you’ll be fine. You don’t need very much power to pull a dent in hot steel, so a small 3- to 5-pound slide hammer is perfect for this job. A large crease may warrant a heavier slide, however.
- Oxyacetylene torch with rosebud tip
- Stud welder (preferred) or MIG welder
- 2-3mm weld studs
- Slide Hammer (5-pound is sufficient)
- Straightedge
- Body hammers
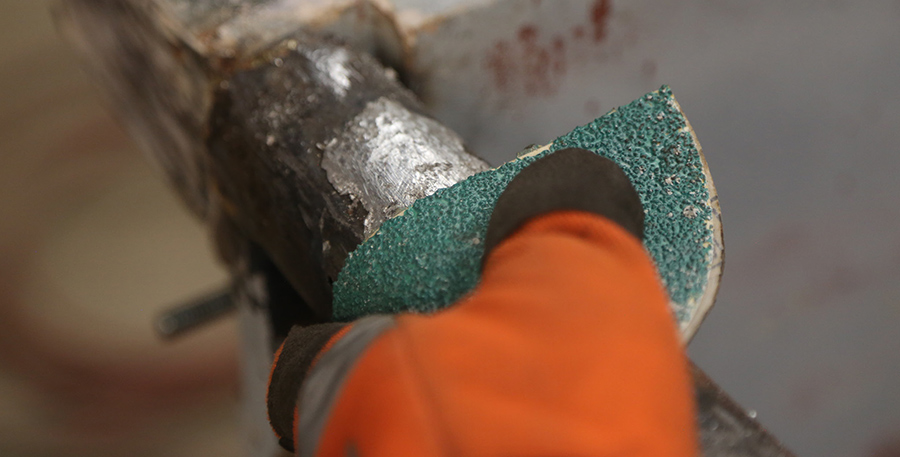
- Grinder/sander with 50-grit disc
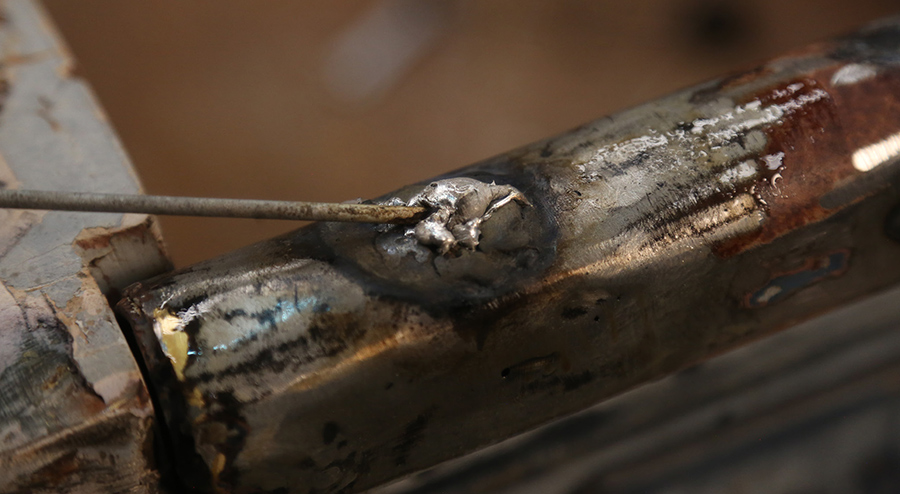
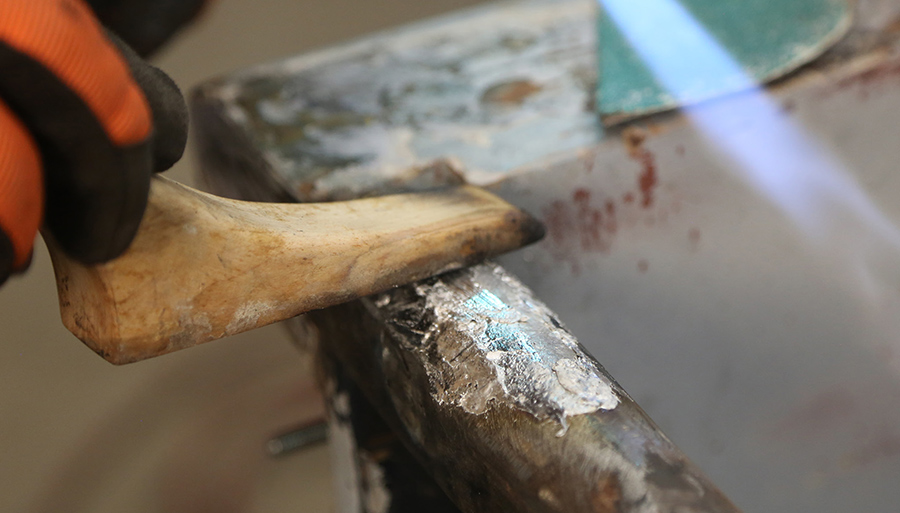
We used the same torch for the body solder. The keys to body solder are to use just enough heat to make the solder flow but not melt. You will melt a bit here and there, but you’ll figure out how to properly heat the solder in less than 5 minutes of working with it. Lead-free solder is the best solution, as it is not as toxic as lead (you still want to avoid breathing the dust) and stays “plastic” longer, from 430- to 930F, whereas lead is only “plastic” (spreadable) between 535- to 660F.
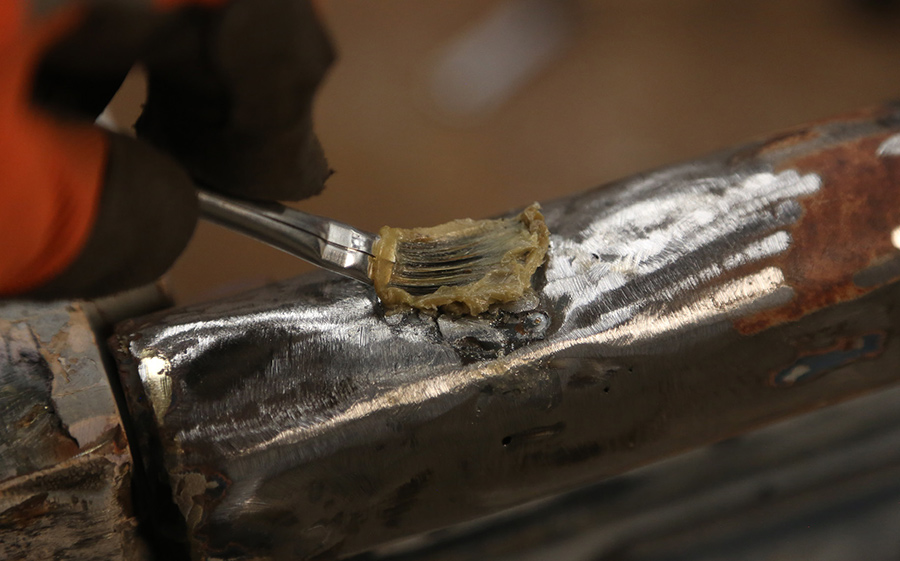
The same flux works for both lead and lead-free solder. Flux is brushed on and then the metal is heated until the flux flows out and then wiped clean. Solder only sticks to fluxed areas, so you have to take care that the entire repair area is fluxed. Body solder is an under-utilized material for repair and custom projects; it is harder to use, but it lasts forever, doesn’t rust, can’t absorb moisture, and has more “give” than plastic fillers, so it can take more impact without cracking or separating from the base metal.
- Lead-free body solder
- Tinning butter with acid brush
- Wooden spreader spoons
- Body files
- Oxyacetylene torch
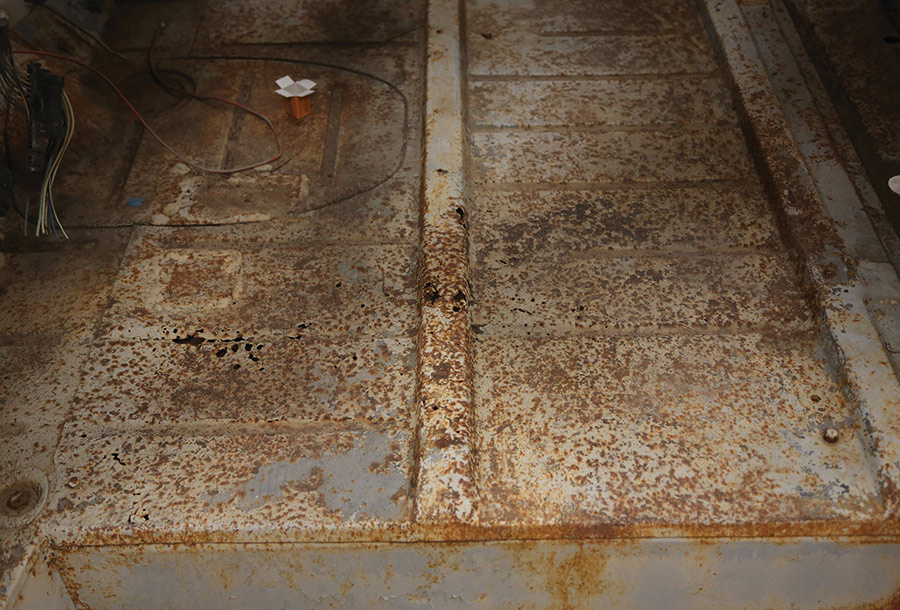
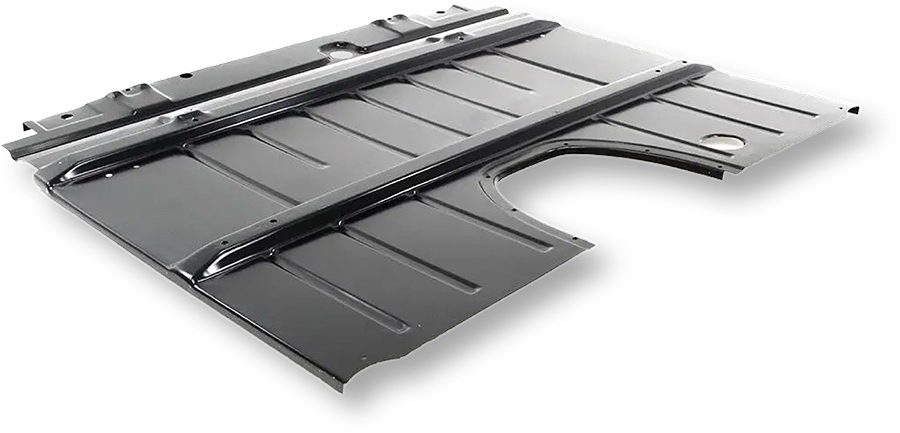
The floorpans in this truck are not terrible; in fact, there is just a bit of through-rust on the driver side and that’s about it. If these floors were completely rotten, we would just order up a set of new stampings from Auto Metal Direct (AMD), but ours only needed a relatively small area repaired. The only way to get the pieces we need is to either buy a complete floorpan for $200 and scrap most of it or install the whole thing, which is much more work. We opted to show you how to fab a quick floor patch so you can spend your hard-earned money on things like fenders and bedsides.
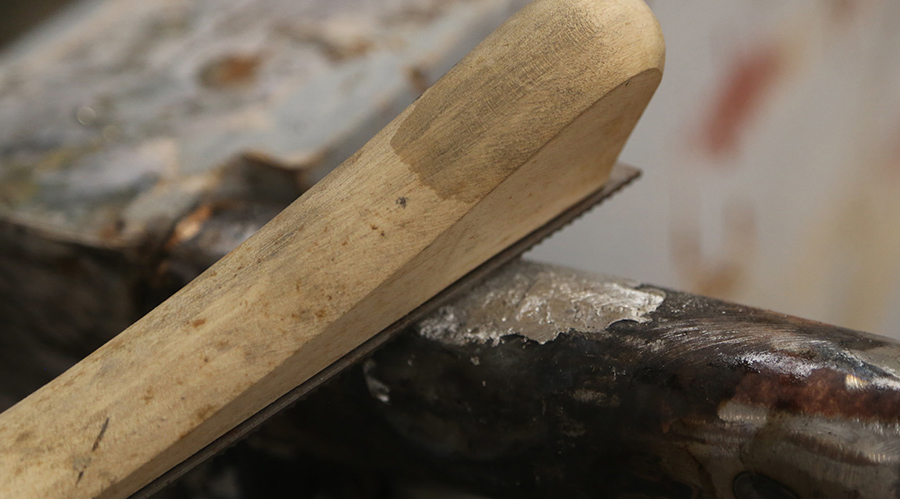
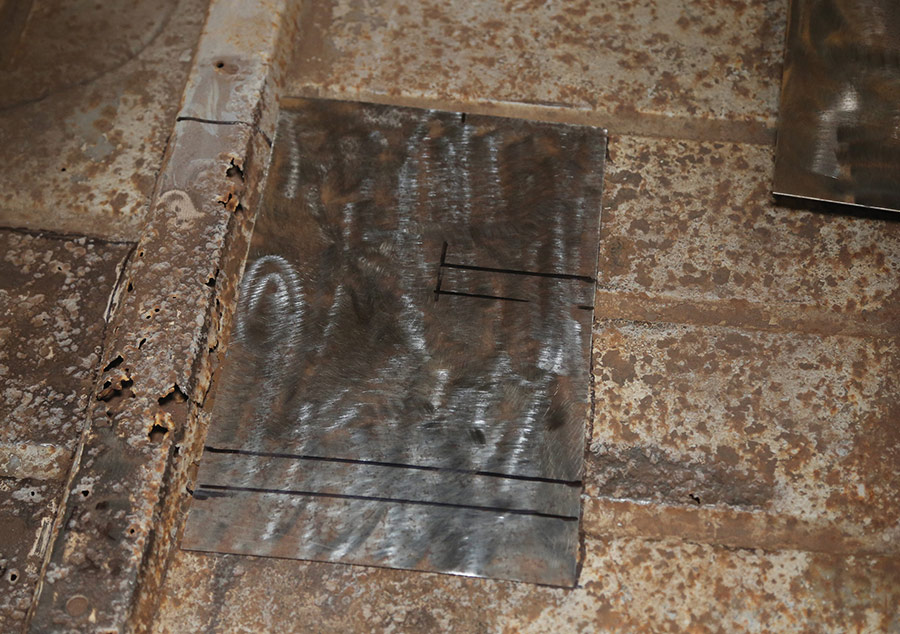
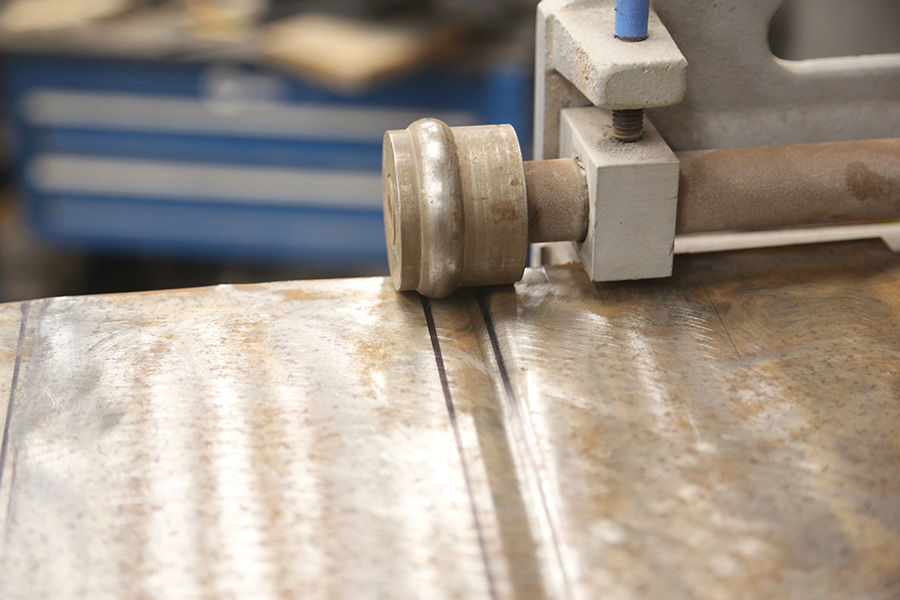
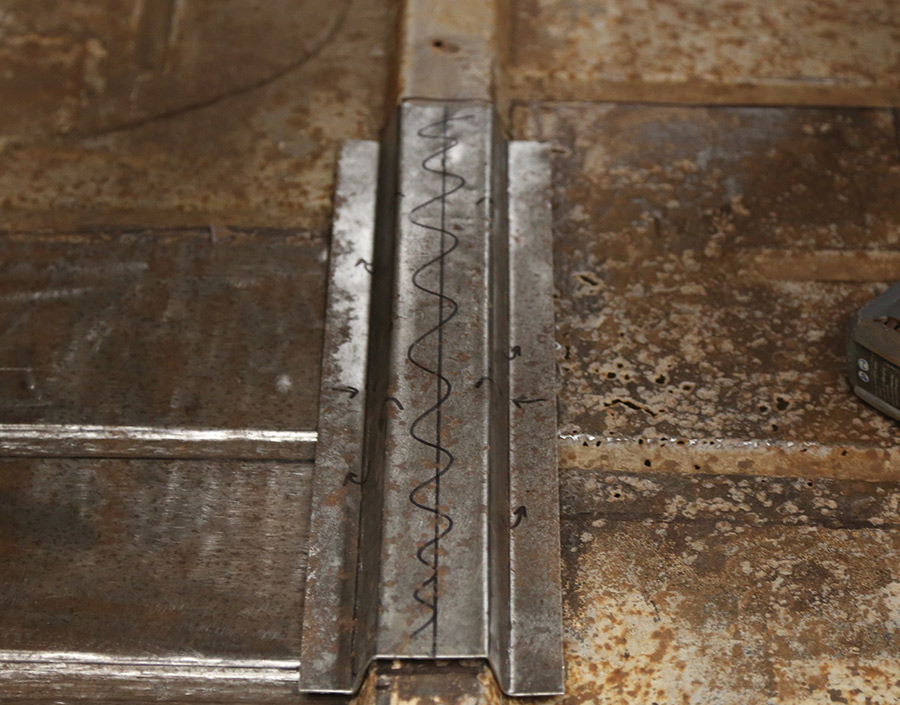
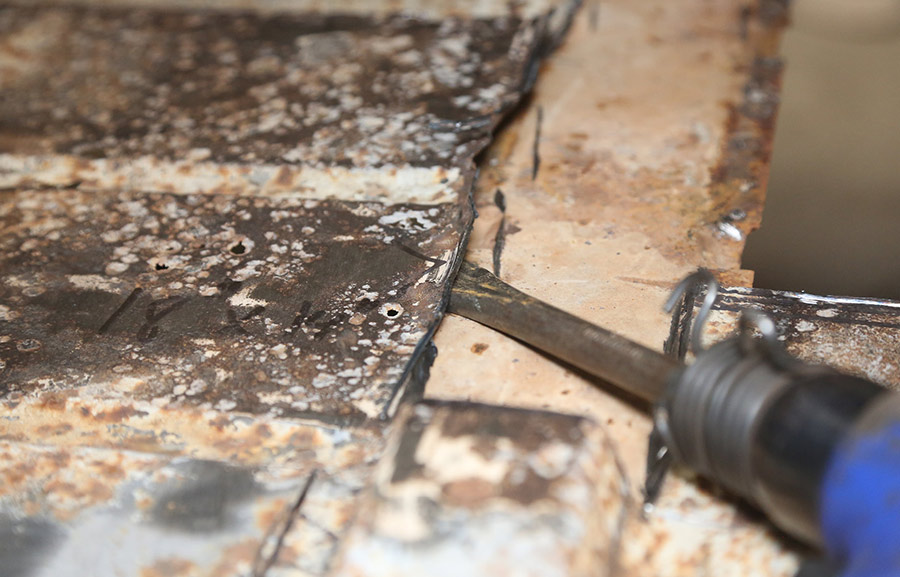
You might be tempted to use flat sheet as-is, however the floor would have very little strength and would be quite floppy. Instead, you need to add ribs that match the original floorpan. While we have a full complement of sheetmetal fab tools, you do not need them to make these basic panels. You can have your sheet sheered at the metal supply, or use a cut-off wheel, so that’s easy. The hardest part is the ribs. There are ways of doing this without specialty tools, but a bead roller is the fastest way to do it. You can buy a cheap hand-crank bead roller for less than $200, which is best used with a partner (one to crank, one to feed the sheet), or add a motor and pedal for another couple hundred bucks. Alternatively, you can hand form the ribs using a piece of iron pipe as a dolly.
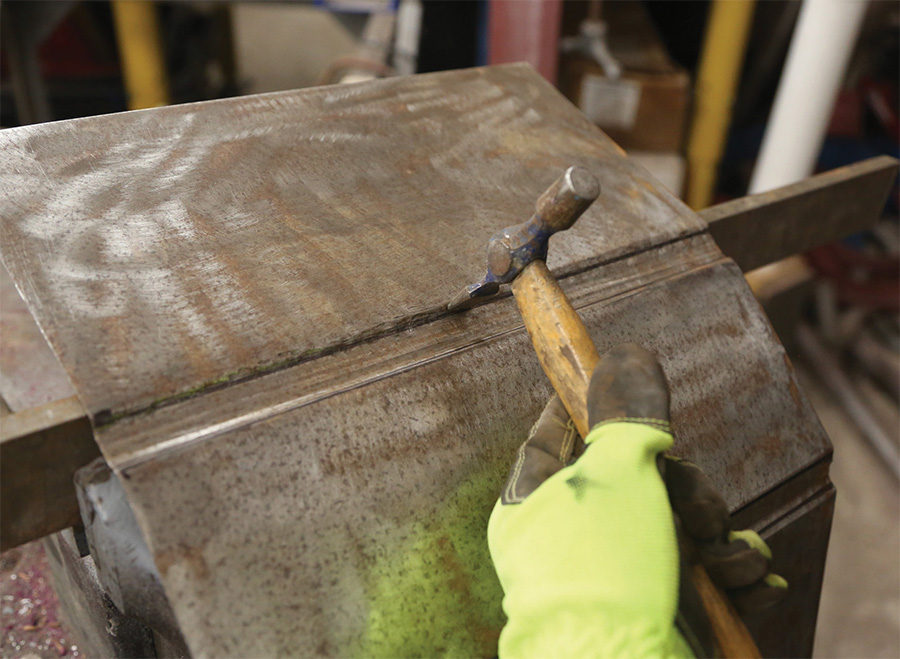
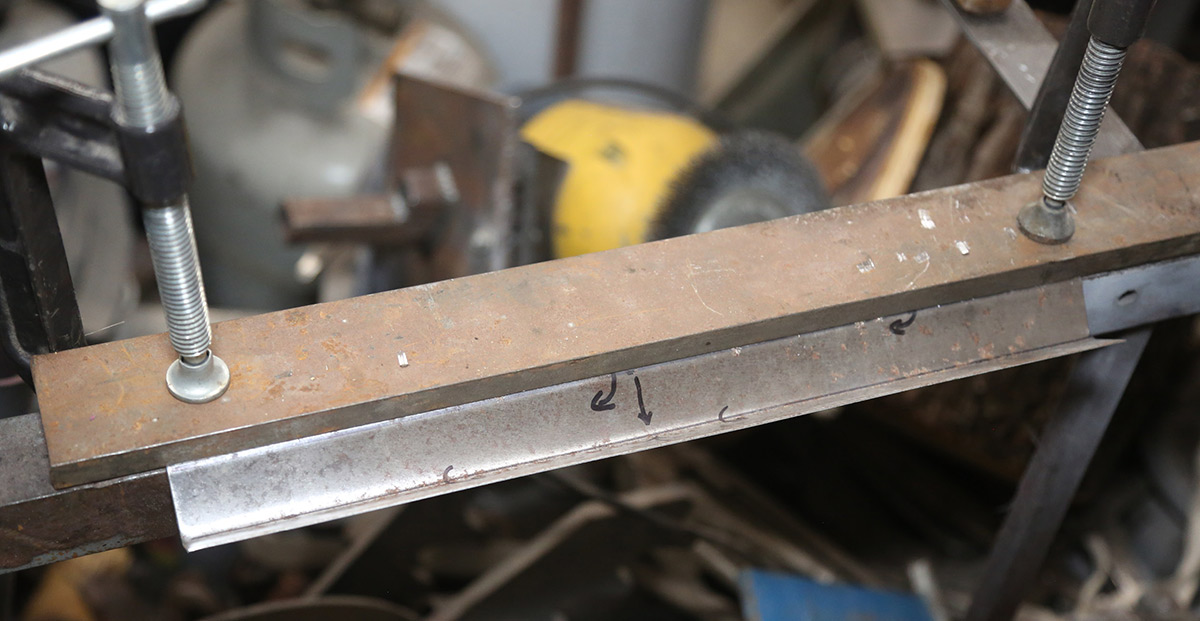
Everything else we used you likely already have. We have a sheet metal brake, but we opted to use a workaround that most garages have: a hard-edged bench, a couple clamps, a strip of 3/8-inch-thick plate, and hand formed the bends. Benchtop brakes are cheaper than bead rollers, but we want to show some alternatives to having the “right” tools. You can use almost any hammer for this job, but the best hammer for refining the ribs is a chasing or chisel hammer with a wide, thin tip. This helps define the edges of the rib so it looks factory. It won’t be quite as crisp as a press-formed sheet, but it is also on the floor, under the carpet, so only you know what it looks like.
- 18-gauge sheet metal
- Cut-off wheel/tin snips
- Grinder and sanding discs
- Bead roller or shaping block (3/8-inch steel plate works well)
- Bench vise
- Welder
- Body hammers (chasing or chisel preferred) Marker
- Measuring tape/ruler
- Weld-through coating
- Primer
- Punch/flange tool (optional)
- Small- to medium-size Locking clamps
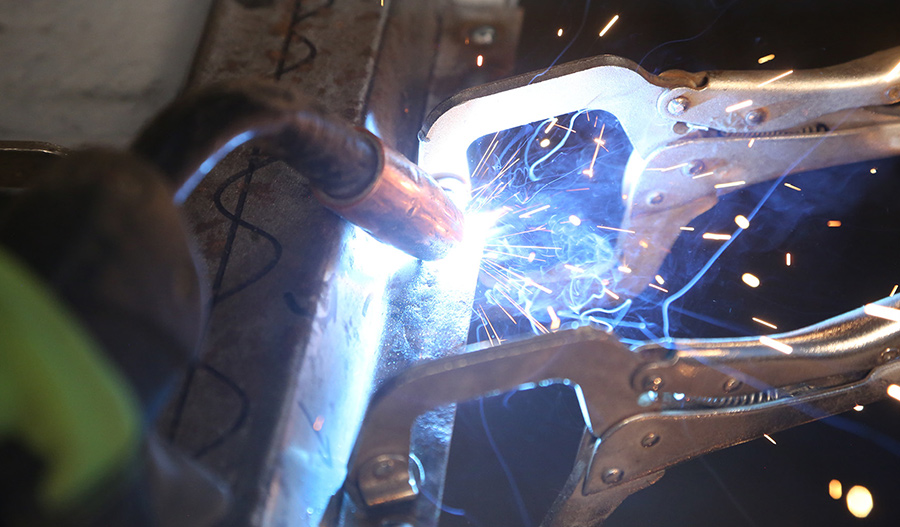
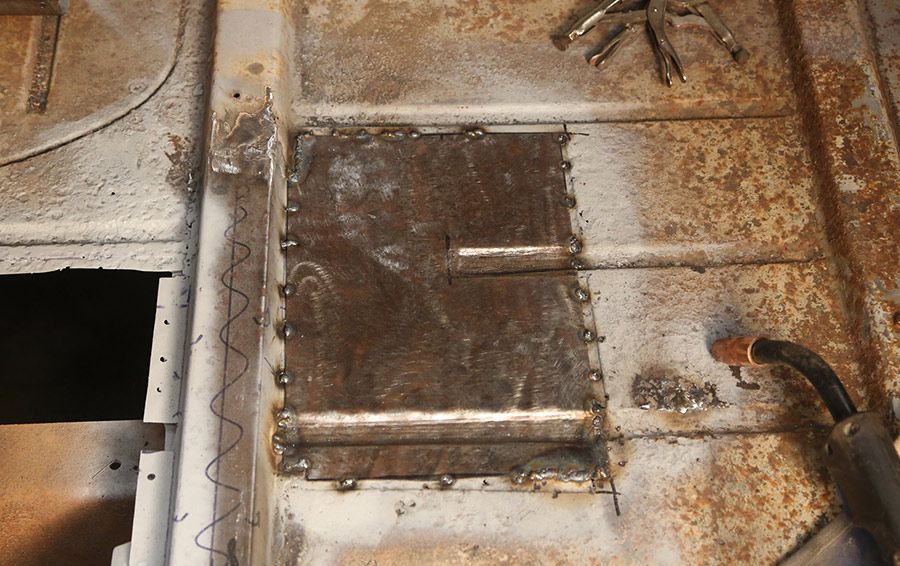
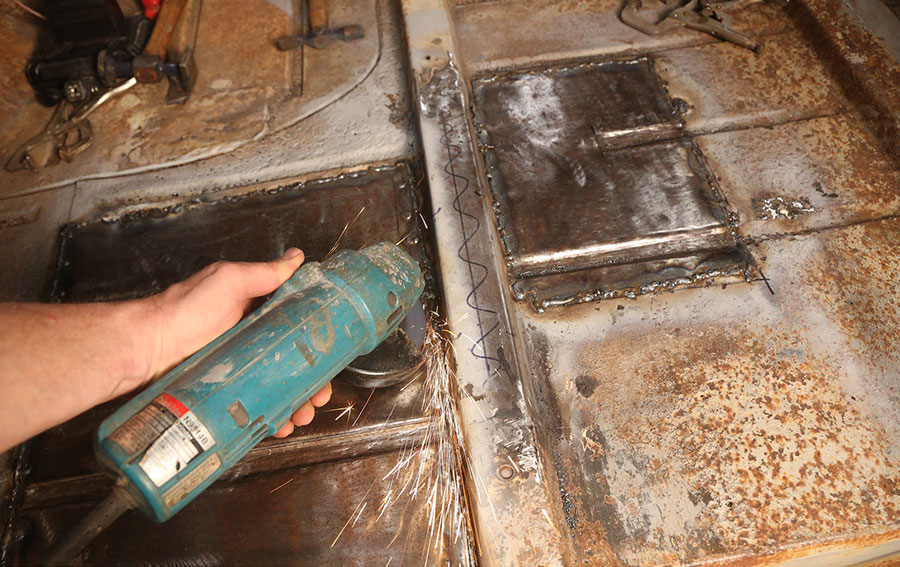
We used a sheet of 18-gauge sheet steel to create our panels. We made three separate panels, the front floor, rear section, and the centerbrace. All required ribs or bends, but nothing crazy, just basic straight ribs and bends. We fabricated the patch panels, cut out the floor, and prepped the metal for welding in about 4 hours, then spent about 3 hours doing the final fitment and welding. If you have never done it before, plan on about 2 days of work for a job this big, but you may be done faster.
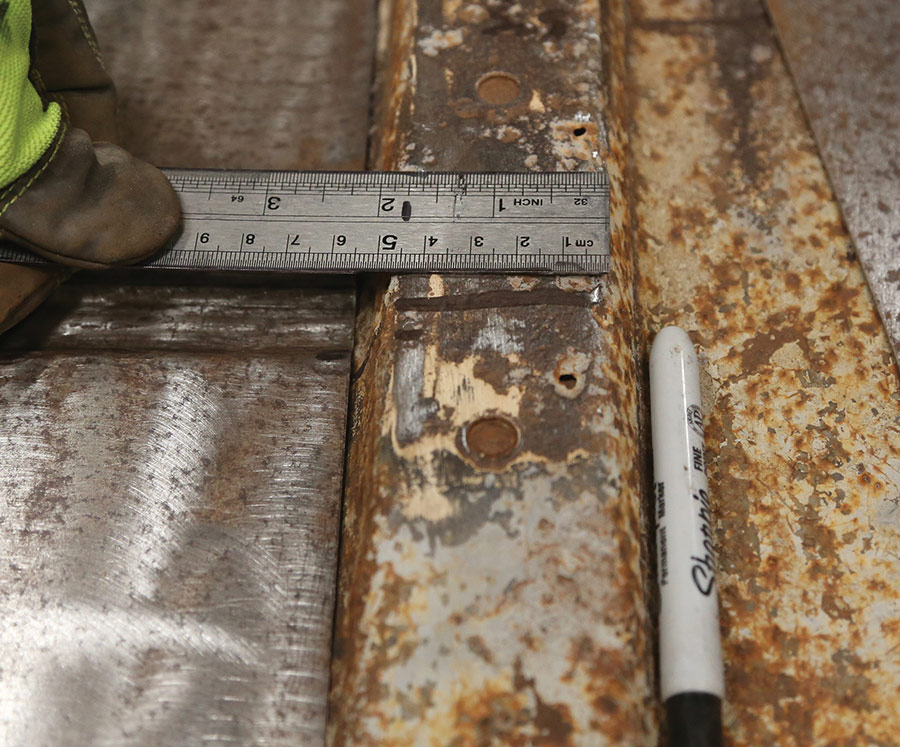
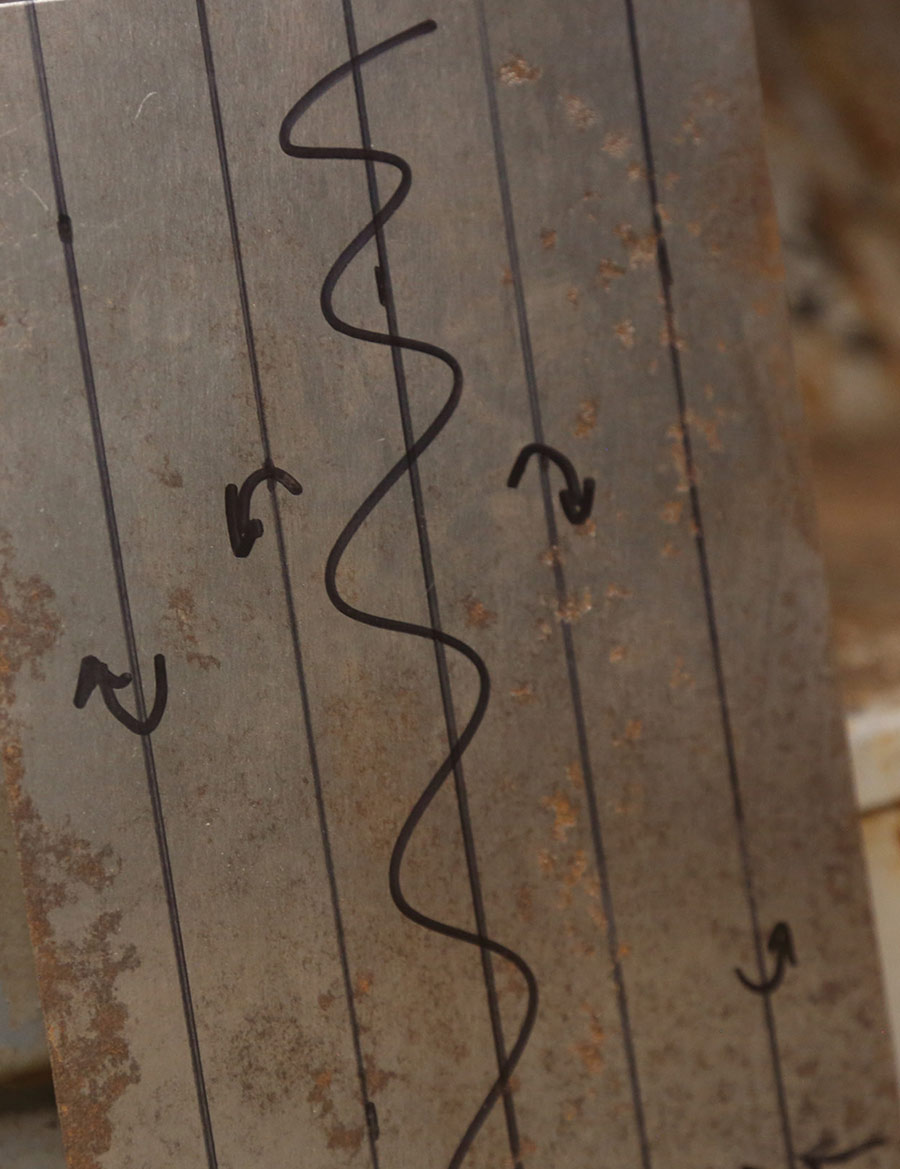
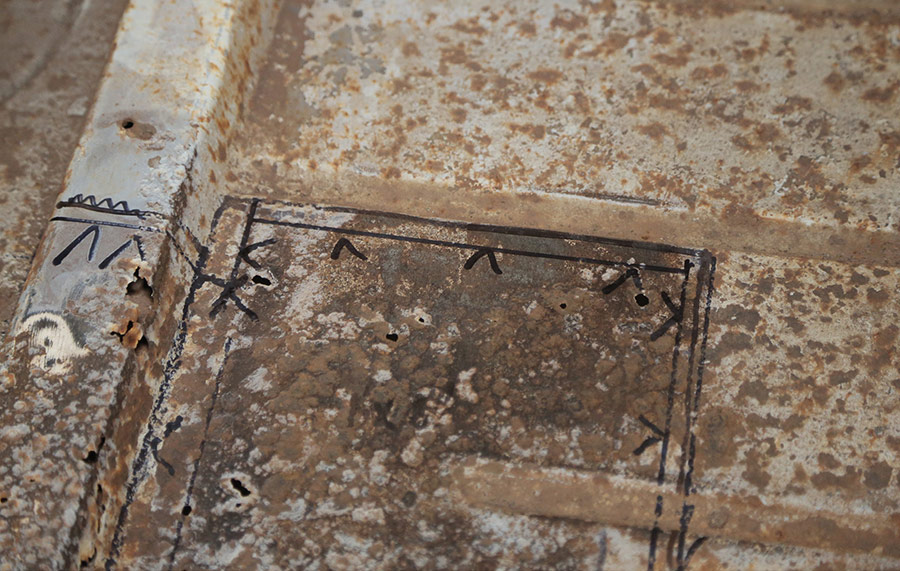
The keys to a good fabrication job are careful measurements and notes. We make notes on the lines for bends indicating the direction of the bend (up or down), which saves you a lot of remakes. Check the fit repeatedly until you are satisfied with the results, then mark the placement of the panel on the floor. It is incredibly easy to make a panel fit and then install it 1/8-inch out, and it screws up the alignment by an inch in another place, so be careful, pay attention, and don’t start welding until you are ready.
You could certainly buy the full floor and cut it up or install it whole, but that is definitely going to take longer than a day. We spent $10 on the sheetmetal, everything else we already had. To get both of these areas in new metal would have cost about $400 with shipping ($199 panel, $189 shipping). Is this method perfect? No, it isn’t, but you get to practice metal forming and that $390 is still in your wallet, which you can spend on new AMD exterior sheetmetal. Regardless of whether you buy or build your floor patch, the process is the same. Now let’s go ruin some perfectly flat sheet metal.





autometaldirect.com